
 Abosh
Line balancing assigns work elements to stations so each station’s load fits within takt time. Theoretical minimum operators = total work content ÷ takt, rounded up. With 3.5 minutes of work and a 1.75-minute takt, the arithmetic says two operators. But no split of these five elements keeps both operators under takt, so three are needed. Do not balance every station to 100%: leave room for variation, recovery and quality checks.
A worked example with five work elements and a stated takt
The reason the arithmetic minimum is often infeasible
Why a perfectly even balance is the wrong target
Start with takt and total work content
Line balancing is the process of distributing work elements across stations or operators so that no station needs more time than takt allows. Two numbers frame it: takt time and the total work content of the product.
For the takt calculation and how it differs from cycle and lead time, see takt time vs cycle time vs lead time.
Round up. Treat the result as a lower bound, not a plan.
Worked example: 240 units per shift
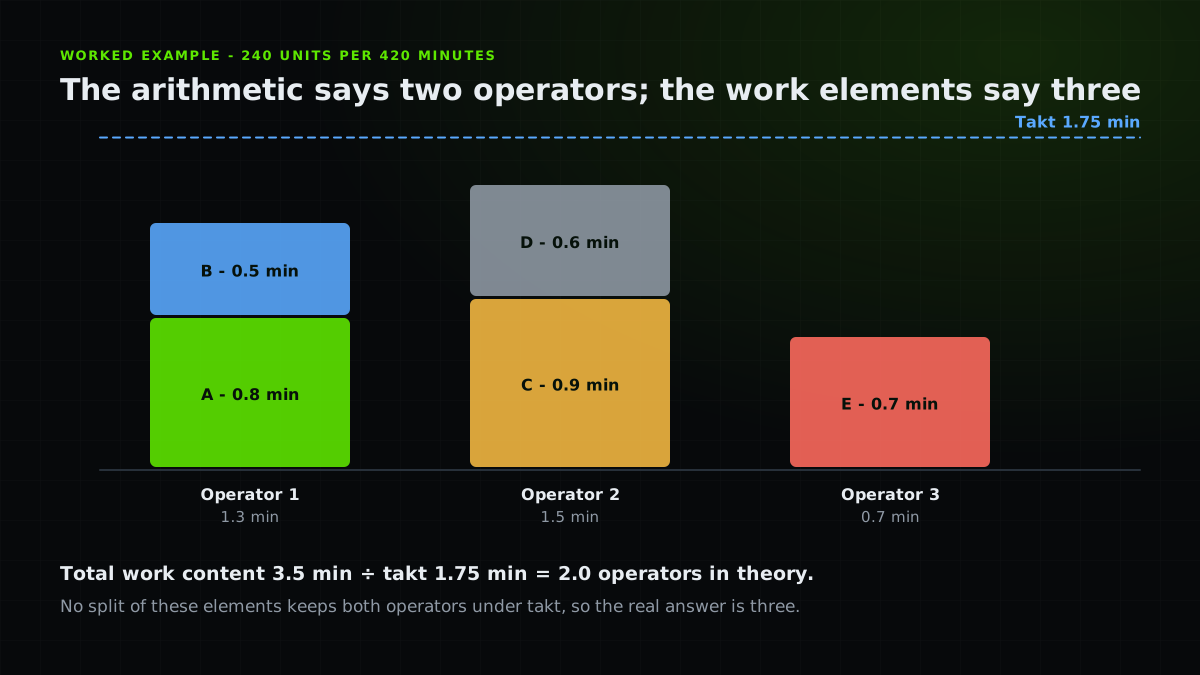
Demand is 240 units per shift and available time is 420 minutes, so takt is 420 ÷ 240 = 1.75 minutes per unit. The product has five work elements: A = 0.8, B = 0.5, C = 0.9, D = 0.6 and E = 0.7 minutes. Total work content is 3.5 minutes.
The theoretical minimum is 3.5 ÷ 1.75 = 2 operators. That looks efficient, and it is not achievable here.
| Element | Time (min) | Cumulative (min) |
|---|---|---|
| A | 0.8 | 0.8 |
| B | 0.5 | 1.3 |
| C | 0.9 | 2.2 |
| D | 0.6 | 2.8 |
| E | 0.7 | 3.5 |
Why two operators do not work
With two operators, each must carry exactly 1.75 minutes to stay within takt. No combination of these elements adds up to 1.75. The closest split is A + C = 1.7 and B + D + E = 1.8, which leaves one operator 0.05 minutes over takt. If the elements must also follow the order A to E, the split is worse: the first operator can hold A and B, leaving 2.2 minutes for the second.
A 1.8-minute station cycle produces at most 420 ÷ 1.8 = 233 units per shift, seven short of demand. Three operators solve it: A and B for the first, C and D for the second, and E for the third, with loads of 1.3, 1.5 and 0.7 minutes.
What the arithmetic leaves out
The formula treats work as infinitely divisible. Real stations are constrained by more than time.
- Precedence: some elements cannot start until others finish.
- Walking, loading and unloading: these add to the operator cycle and are easy to forget.
- Machine time: an operator cannot start a step while the machine is still cycling.
- Ergonomics and safety: two elements may need different postures or tools that cannot share a station.
- Variability: an operator loaded to 100% of takt has no room for a slow cycle or a quality check.
Do not balance every station to 100%
Allow time for normal variation, recovery after a stop, material handling, fatigue and quality checks. A station loaded exactly to takt has no allowance for that work. Check how slower cycles affect the output the customer needs.
Test a task allocation under representative variation. Check which replenishment, quality and response tasks fit safely within the time available at the lighter-loaded station.
- Calculate takt
Use net available time and real demand.
- List elements
Time each work element, including walking and handling.
- Respect precedence
Draw the order in which elements must happen.
- Assign to stations
Keep each load under takt with margin for variation.
- Test on the floor
Time real cycles and adjust. Check where the bottleneck moves.
Common mistakes in line balancing
Before moving tasks between stations, check the observed work times and the restrictions on who can perform each task.
- Using the machine cycle time instead of the full operator cycle.
- Ignoring walking, handling and time spent waiting for a machine.
- Balancing to an old takt after demand has changed.
- Chasing a visually flat bar chart and removing all slack.
- Moving work between stations without checking precedence, ergonomics or quality checks.
A related example from Abolfazl
Compare individual station cycles with demand instead of trusting their average.
In English, on founder Abolfazl’s personal blog. This is related reading, not an independent technical source.
Practical checklist
- Calculate takt from net available time and real demand.
- Time every work element, including walking and handling.
- Write down precedence constraints before assigning work.
- Treat total work content ÷ takt as a lower bound.
- Check whether any combination of elements can actually fit the operator count.
- Leave margin on every station for variation and recovery.
- Give the lightest station the work that protects flow.
- Re-time cycles on the floor and check where the bottleneck moves.
FAQ
FAQ
Sources and further reading
Authoritative references used to research and verify this guide.