
 Abosh
Heijunka levels production quantity and product mix over a defined period. Start with a credible demand mix, translate it into container quantities, then build a repeating sequence the process can execute. Check production, changeover, material and staffing capacity before releasing the pattern. Leveling can reduce uneven upstream demand, but it does not remove customer variation or justify producing unwanted stock. Keep a stated replenishment policy and revise the pattern when its assumptions change.
Turn a product mix into a checkable repeating sequence.
Budget processing and setup time before committing.
Recognize when repetitive leveling is the wrong release rule.
Fictional AABC allocation, with demand, container quantity, time allowances and twelve release slots.
CSVBlank heijunka boxEnter your own inputs and allocation. Redraw the grid if the slot count changes; no automatic calculation.
Level a real mix over a stated period
The Lean Enterprise Institute defines heijunka as leveling the type and quantity of production over a fixed period. Producing all of A on Monday and all of B on Tuesday can send lumpy requirements upstream even when average demand looks balanced.
A repeating sequence spreads that requirement more evenly. It depends on replenishment stock, feasible changeovers and a reasonably useful demand pattern. The customer’s orders can still arrive unevenly.
This guide builds the pattern. SMED addresses setup reduction, and production scheduling covers wider constraints.
Convert demand into manageable containers
Illustrative planning window: four working hours, with demand for 120 units of A, 60 of B and 60 of C. Each container holds 20 units. The requirement becomes six A containers, three B containers and three C containers.
AABC repeated three times gives exactly those 12 containers. Each four-slot cycle releases 80 units in the required 2:1:1 ratio. The sequence is an example, not a claim that it is the best order for every machine.
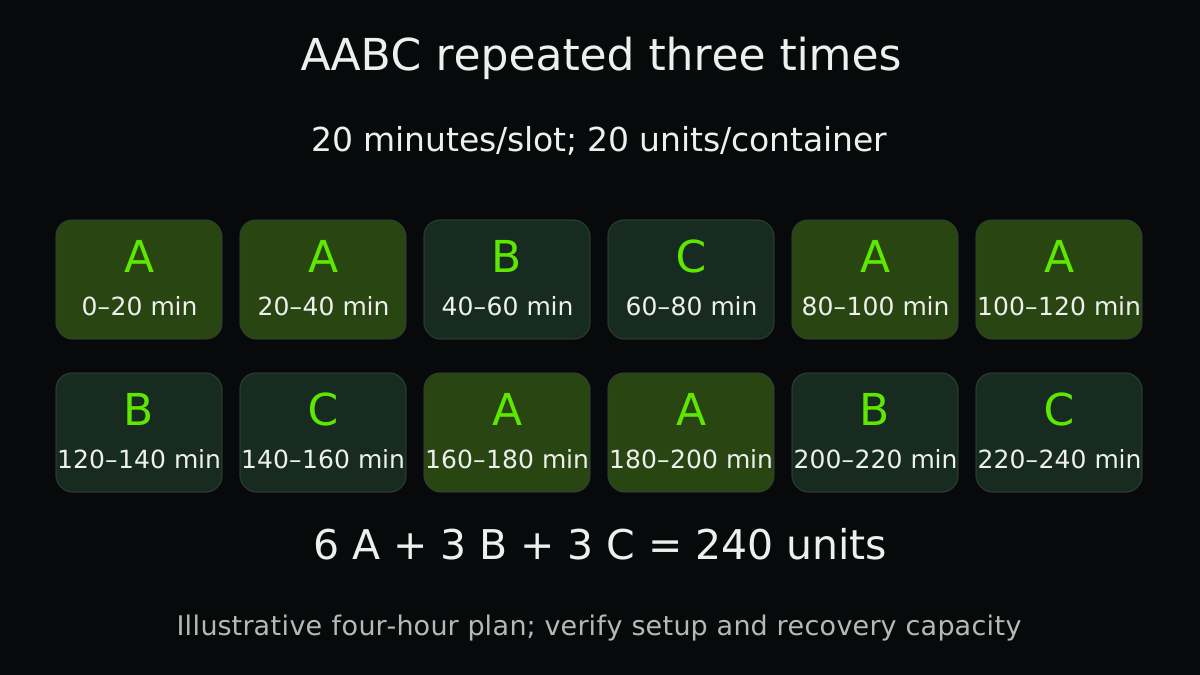
| Product | Units in window | Units/container | Containers |
|---|---|---|---|
| A | 120 | 20 | 6 |
| B | 60 | 20 | 3 |
| C | 60 | 20 | 3 |
| Total | 240 | 20 | 12 |
Fill in the box, then check whether the plan can run
The fictional box below uses one row per product and one column per release slot. Four hours must cover 120 units of A, 60 of B and 60 of C. At 20 units per container, that means six, three and three containers. AABC repeated three times fills twelve slots.
Each slot allows 20 minutes: 15 for processing and five for the assumed setup and handling allowance. All 240 minutes are allocated. There is no spare capacity. Matching the arithmetic does not prove that the sequence, material, staffing or replenishment can support it.
Download the filled box to inspect the allocation. Use the blank file for your own demand, container quantities and times. If the required slot count changes, redraw the grid rather than forcing the job into twelve slots. The CSV is editable; it does not recalculate or approve a schedule.
The four-hour planning window differs from the time between successive runs of a product. EPEI and product wheels explain that repeat interval and its setup constraint. A filled box still needs an agreed consumption and release rule.
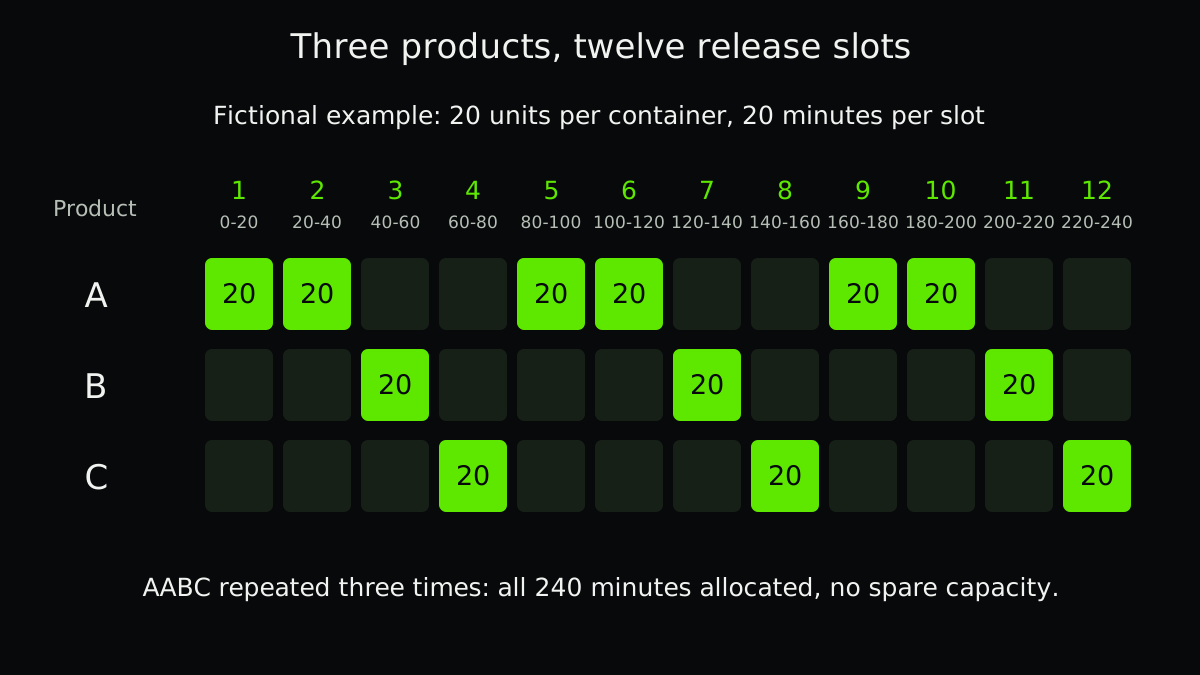
| Product | Containers | Units | Release slots |
|---|---|---|---|
| A | 6 | 120 | 1, 2, 5, 6, 9, 10 |
| B | 3 | 60 | 3, 7, 11 |
| C | 3 | 60 | 4, 8, 12 |
Check pitch against the available minutes
For this example, each container needs 15 minutes of processing. Reserve up to five further minutes per slot for changeover and handling. Twelve slots × 20 minutes = 240 minutes. That budget fits exactly, leaving no unallocated recovery margin.
The five-minute allowance is deliberately conservative and simplified, including A-to-A slots. A real schedule should use measured sequence-dependent setups and explicitly budget cleaning, maintenance and interruptions. If a B-to-C change actually takes 18 minutes, this pattern is infeasible.
Pitch here means the time allocated to one container release. It is not the same as unit cycle time. The takt and cycle-time guide explains the clocks.
Define how the box authorizes each release
A heijunka box distributes release signals by time and product. Whether physical or digital, it needs a rule for missed slots, urgent orders and unused authorizations.
A cancelled consumption signal should not become unwanted production merely because an empty slot looks untidy. Connect the schedule to the chosen pull policy and kanban loop.
- Choose the planning family
Group products sharing a feasible process and state the demand window and inventory policy.
- Calculate containers and sequence
Translate required units into releases; reconcile the proposed pattern back to each product total.
- Prove capacity and replenishment
Test actual processing, sequence-dependent setup, materials, people and the time to usable replacement stock.
- Define exceptions and review
Specify missed-slot response, authorized resequencing and the trigger for revising the demand pattern.
Keep high-mix and make-to-order limits visible
Rare jobs, expensive stock, unpredictable product combinations or very long setups can make a fixed small-container pattern unsuitable. Leveling at product-family level or a different release policy may serve the customer better.
The interval between runs of a product also affects required replenishment inventory. Smaller batches can reduce that interval, but frequent setups consume capacity. Test both consequences rather than assuming more switching is always lean.
A good review includes stockouts, inventory age, setup effort and actual customer delivery. Schedule regularity by itself is not the outcome.
Review the pattern when the mix changes
If demand becomes A = 60, B = 120 and C = 60, the old AABC pattern overproduces A and under-supplies B. Preserve the original assumptions so the team can see why it no longer fits.
Use exception records to improve the next pattern. Separate a genuinely changed demand mix from a one-off disruption and retain a feasible near-term plan while replanning.
A related example from Abolfazl
Compare level quantity with uneven demand and the stock needed between days.
In English, on founder Abolfazl’s personal blog. This is related reading, not an independent technical source.
Practical checklist
- State the product family and planning window.
- Check whether demand supports replenishment stock.
- Convert units into explicit container sizes.
- Reconcile sequence totals by product.
- Budget measured processing and setup times.
- Include interruptions and replenishment delays.
- Assign missed-slot and urgent-order rules.
- Review customer service, inventory and setup effort together.
FAQ
FAQ
Sources and further reading
Authoritative references used to research and verify this guide.